

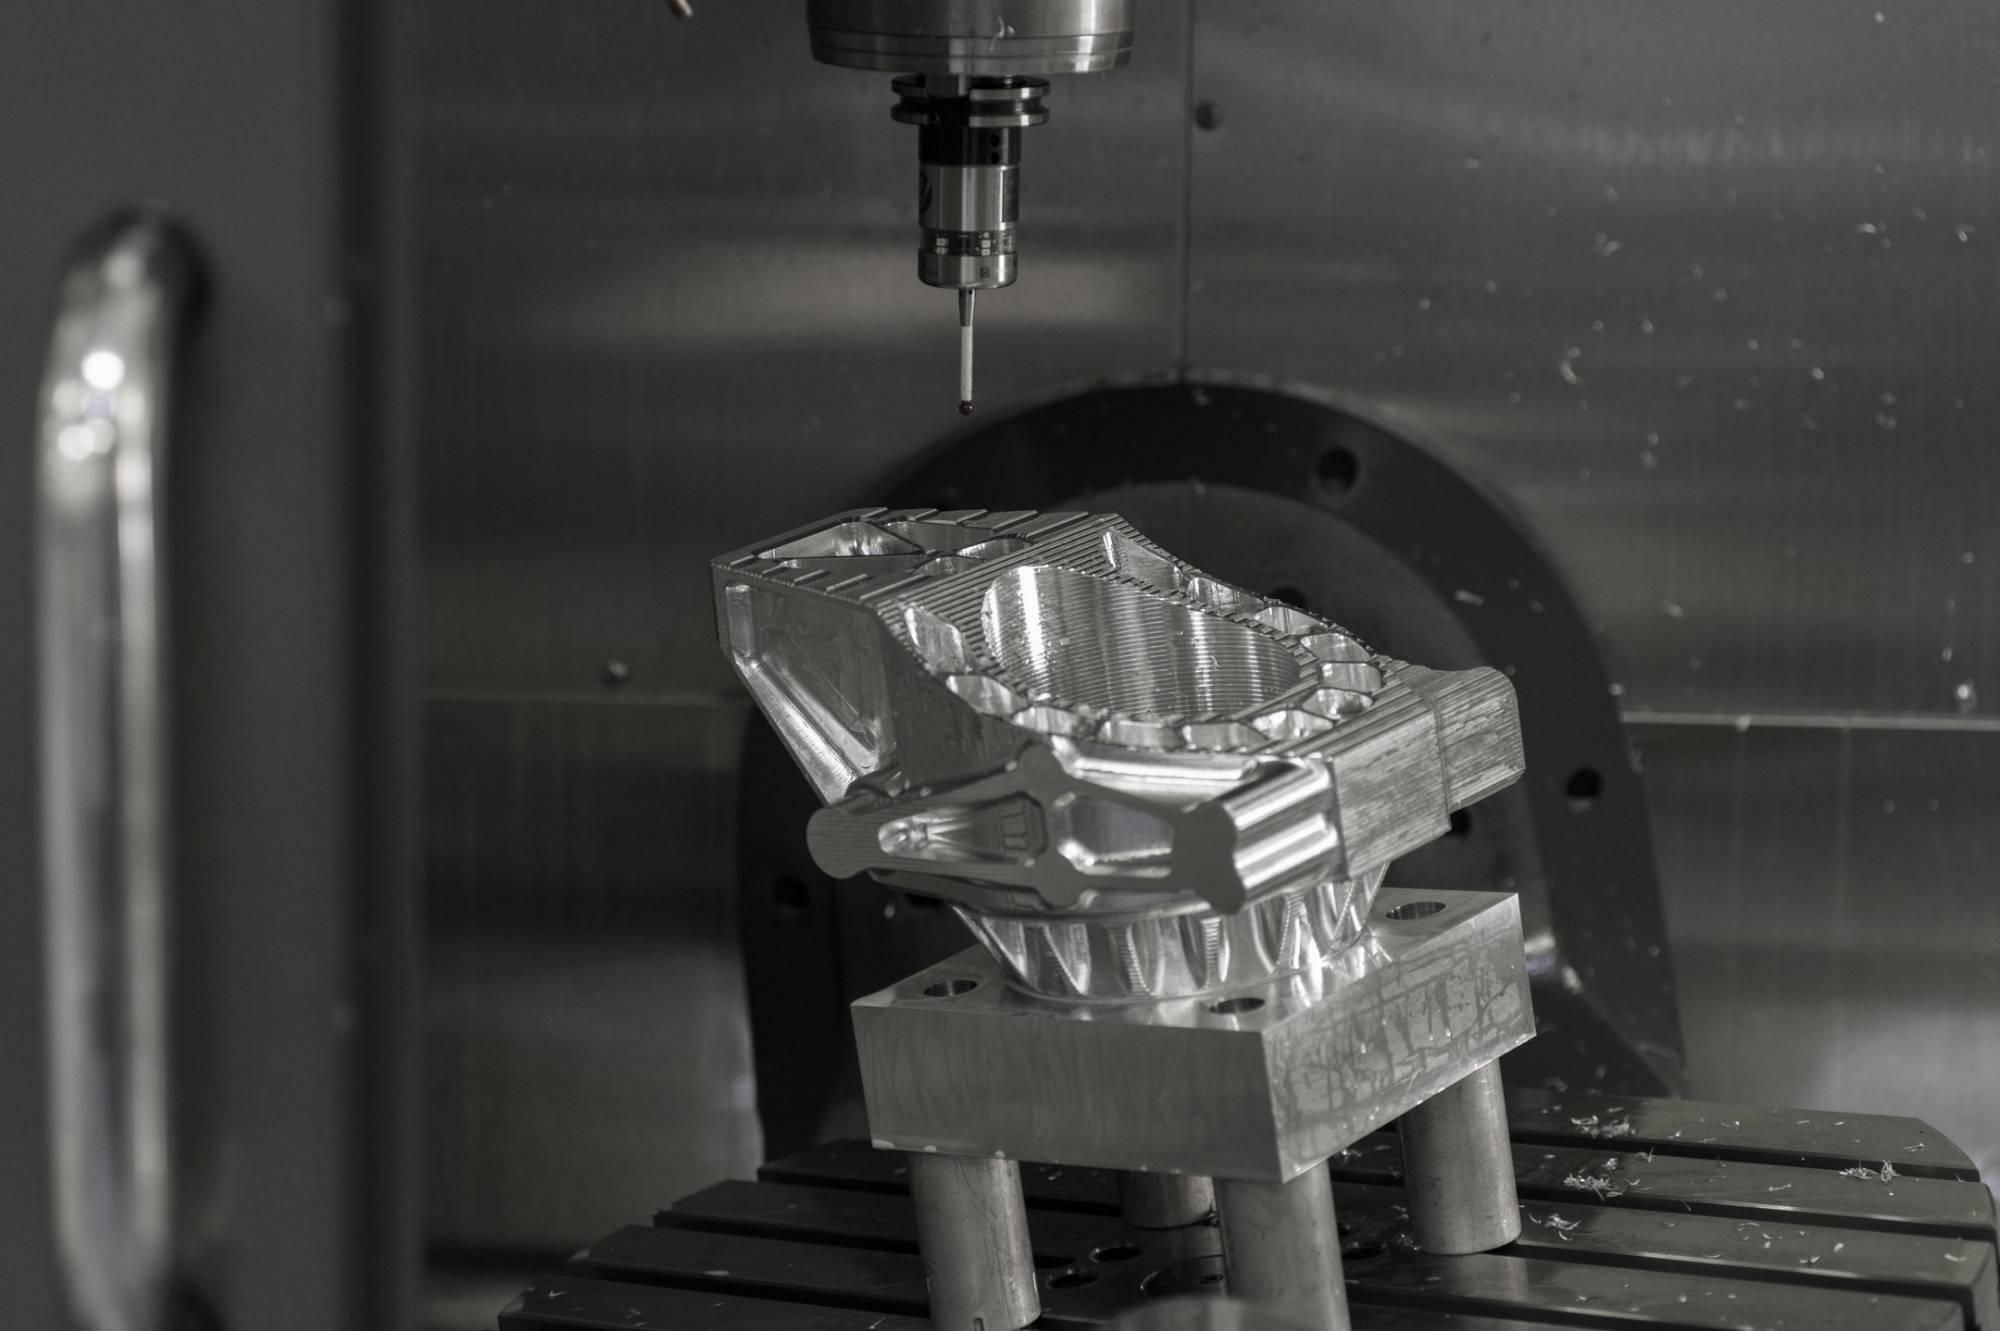
Magnesium is one of the lightest structural metals used in modern manufacturing. With its low density, good strength-to-weight ratio, excellent machinability, and effective heat dissipation, magnesium alloys are widely used in aerospace, automotive, electronics, medical equipment, robotics, and precision industrial components.
However, how to machine magnesium correctly is an important question for manufacturers and engineers. Although magnesium is generally easier to cut than many aluminum alloys, steels, and titanium alloys, improper machining conditions can create problems such as excessive heat, poor surface finish, dimensional variation, chip accumulation, and, most importantly, fire hazards caused by fine magnesium chips or dust.
This guide explains the key principles of Magnesium Machining, including CNC milling, turning, drilling, cutting tool selection, chip control, cooling methods, and machining safety.
Is Magnesium Easy to Machine?
Yes. Magnesium and many magnesium alloys have excellent machinability.
Compared with steel, stainless steel, and titanium, magnesium requires relatively low cutting forces. This allows manufacturers to achieve higher machining productivity while reducing tool wear and spindle load.
The main advantages of Machining Magnesium Alloy include:
Low cutting resistance
High possible material removal rates
Good dimensional accuracy
Excellent surface finish
Relatively low cutting-tool wear
Reduced machine power requirements
Suitable for high-speed CNC machining
For these reasons, CNC machining magnesium can be highly efficient for both prototypes and high-volume production.
However, the excellent machinability of magnesium does not mean the machining process can be treated exactly like aluminum machining. Chip control, heat management, dust collection, and fire prevention require special attention.
What Magnesium Alloys Can Be Machined?
Most commercially available magnesium alloys can be machined using CNC equipment.
Common alloys include:
| Magnesium Alloy | Main Characteristics | Typical Applications |
|---|---|---|
| AZ31 | Good formability and machinability | Electronics, panels, structural parts |
| AZ61 | Higher strength than AZ31 | Mechanical components, housings |
| AZ80 | High strength and good machinability | Aerospace and automotive parts |
| AZ91 | Good castability and mechanical properties | Gearboxes, housings, automotive components |
| ZK60 | High strength-to-weight ratio | Aerospace and high-performance components |
| WE43 | High-temperature performance | Aerospace, motorsport, medical applications |
The correct Magnesium Alloy Machining strategy depends on the alloy composition, component geometry, tolerance requirements, and final surface treatment.
How to Machine Magnesium
A successful magnesium machining process should focus on four major areas:
Selecting suitable cutting tools
Maintaining efficient cutting conditions
Removing chips quickly
Controlling heat and ignition risks
Modern CNC machining centers, milling machines, turning centers, and drilling machines can all be used to manufacture magnesium components.
1. Select the Right Cutting Tools
Sharp cutting tools are essential when machining magnesium.
Because magnesium is relatively soft, dull tools can generate unnecessary friction and heat instead of producing clean chips.
Carbide cutting tools are commonly used for CNC magnesium machining because they provide good edge stability and wear resistance.
Important tool characteristics include:
Sharp cutting edges
Positive rake angles
Good chip evacuation geometry
Proper clearance angles
Minimal tool runout
High-speed steel tools may also be suitable for certain drilling and low-volume machining operations.
The objective is to cut magnesium efficiently instead of rubbing against the workpiece.
Magnesium CNC Milling
Magnesium milling is one of the most common manufacturing methods for producing housings, brackets, aerospace components, electronic enclosures, heat-dissipation structures, and lightweight mechanical parts.
CNC milling can create:
Pockets
Slots
Thin walls
Cooling structures
Mounting holes
Complex three-dimensional surfaces
Precision mating surfaces
Because magnesium generates relatively low cutting forces, high-speed machining can often be used effectively.
However, manufacturers should avoid excessive tool engagement that could generate unnecessary heat.
Good magnesium milling practice includes:
Using sharp milling cutters
Maintaining stable tool engagement
Preventing chip recutting
Using effective chip evacuation
Avoiding excessive dwell
Maintaining appropriate feeds and spindle speeds
Chip recutting is particularly undesirable because repeated cutting can break chips into smaller particles and increase heat generation.
Magnesium CNC Turning
Magnesium turning is commonly used for cylindrical and rotational components such as:
Shafts
Bushings
Sleeves
Connectors
Rings
Precision mechanical components
During CNC turning, tools should remain sharp and stable to produce continuous and predictable cutting conditions.
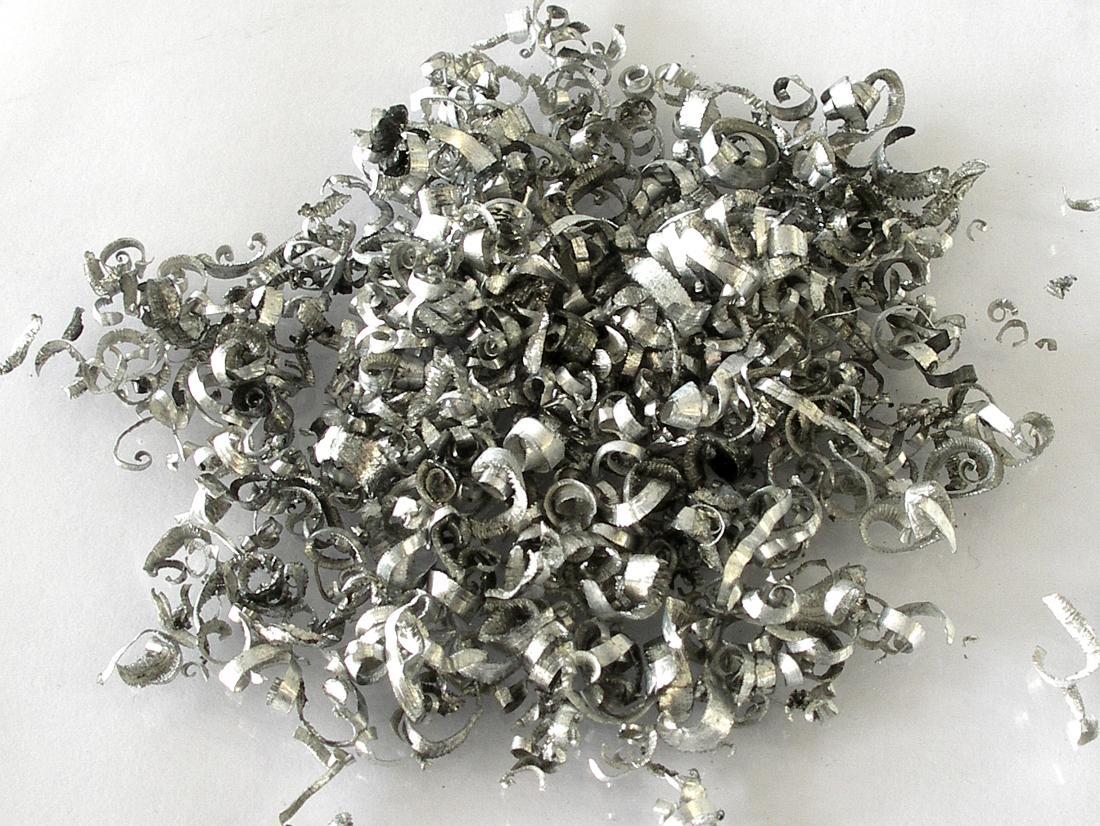
Proper feeds and cutting depths can help form larger chips rather than extremely fine particles.
Fine magnesium particles should be minimized whenever possible because they present a greater ignition risk than larger machining chips.
Manufacturers should therefore optimize cutting parameters to maintain productive cutting while controlling chip size and temperature.
Magnesium Drilling
Magnesium drilling requires effective chip evacuation, especially when producing deep holes.
If chips remain trapped inside a hole, friction and temperature can increase.
For deeper holes, chip removal becomes increasingly important.
Good drilling practices include:
Using sharp drills
Maintaining adequate flute clearance
Removing chips frequently
Avoiding excessive friction
Preventing chip packing
Monitoring tool condition
Peck drilling or other chip-breaking strategies may be used when appropriate for deep-hole machining.
For production machining, the drill geometry should be selected according to hole diameter, depth, alloy grade, and machine capability.
Cutting Speed and Feed for Magnesium Machining
One of the advantages of magnesium machining is the ability to use relatively high cutting speeds compared with many other engineering metals.
However, there is no universal cutting speed that works for every application.
Machining parameters depend on:
Magnesium alloy
Tool material
Tool diameter
Milling, turning, or drilling operation
Cutting depth
Machine rigidity
Workpiece geometry
Surface finish requirement
Cooling strategy
Instead of simply maximizing spindle speed, manufacturers should balance speed, feed, and depth of cut to maintain stable cutting and efficient chip formation.
Very light feeds combined with excessive speed may cause rubbing rather than effective cutting, increasing heat generation.
For this reason, production parameters should be established according to tooling manufacturer recommendations and verified through machining trials.
Dry Machining vs Coolant for Magnesium
Another important question is whether magnesium should be machined dry or with coolant.
Both methods can be used under correctly controlled industrial conditions.
Dry Magnesium Machining
Dry machining can simplify certain operations and prevent coolant contamination.
However, the machining area must have effective chip removal.
Compressed-air-assisted chip evacuation or suitable extraction systems may be used depending on the machine and process design.
Manufacturers must ensure that chips do not accumulate around cutting tools, fixtures, machine enclosures, or electrical components.
Magnesium Machining Coolant
When coolant or lubricant is required, the fluid should be specifically compatible with magnesium and the machining process.
A suitable magnesium machining coolant can help:
Reduce friction
Control cutting temperature
Improve surface finish
Extend tool life
Remove chips from the cutting zone
Coolant selection should be based on the magnesium alloy, machining operation, equipment manufacturer recommendations, and applicable workplace safety procedures.
Chip Control Is Critical
Chip management is one of the most important parts of magnesium CNC machining.
Larger magnesium chips are generally easier to manage than fine chips, dust, or powder.
During machining, manufacturers should prevent chips from:
Accumulating inside the machine
Contacting ignition sources
Entering electrical systems
Building up around motors
Collecting inside extraction equipment not designed for combustible metal dust
Machines should be cleaned regularly using procedures suitable for combustible metal chips.
Chip collection, storage, and recycling systems should also be designed specifically for magnesium-containing waste.
Magnesium Machining Safety
Safety is one of the biggest differences between magnesium machining and conventional machining of many other metals.
Solid magnesium components do not normally ignite under ordinary machining conditions. The primary concern is fine magnesium chips, dust, and powder, which have a much larger surface area and can ignite more easily.
Therefore, magnesium machining safety should be integrated into the entire manufacturing process.
Important precautions include:
Keep Cutting Tools Sharp
Dull tools create friction and excessive heat.
Sharp tools reduce cutting resistance and help produce larger, cleaner chips.
Avoid Chip Accumulation
Chips should be removed regularly from the cutting area and machine enclosure.
Large quantities of dry magnesium chips should not be allowed to accumulate near potential ignition sources.
Control Magnesium Dust
Grinding, sanding, polishing, and very fine machining processes can generate magnesium dust.
Combustible metal dust requires appropriately designed collection and ventilation equipment. Conventional dust collection systems may not be suitable.
Keep Ignition Sources Away
Open flames, welding sparks, smoking, and other ignition sources should be kept away from magnesium machining and chip-storage areas.
Use Appropriate Fire-Response Equipment
Facilities machining magnesium should use fire-response procedures and extinguishing equipment designed for combustible metals.
A Class D fire extinguisher or other approved agent intended for combustible metal fires is commonly required for magnesium-related fire risks.
Workers should follow the facility's established emergency procedures rather than using unsuitable extinguishing methods on burning magnesium.
Avoid Excessive Heat During Machining
Although magnesium normally produces less cutting heat than many harder metals, excessive localized temperatures should still be avoided.
Potential causes include:
Dull cutting tools
Improper feeds
Excessive cutting speed
Chip recutting
Poor lubrication
Tool rubbing
Chip packing
Improper grinding processes
Monitoring the machining process and maintaining consistent chip evacuation significantly reduces these risks.
Workholding for Magnesium Components
Magnesium components can sometimes have thin walls and lightweight structures.
Because magnesium has relatively low stiffness compared with steel, excessive clamping forces may deform thin components.
A good workholding system should:
Provide adequate support
Minimize vibration
Prevent component distortion
Maintain dimensional stability
Provide access for chip evacuation
For thin-wall magnesium CNC machining, custom soft jaws, vacuum fixtures, modular fixtures, or dedicated machining fixtures may be used depending on component geometry.
How to Improve the Surface Finish of Machined Magnesium
A good surface finish depends on cutting-tool condition, machine rigidity, toolpath design, feed rate, and chip control.
To improve the surface quality of magnesium parts:
Use sharp finishing tools
Reduce tool runout
Maintain stable machining conditions
Avoid chip recutting
Use appropriate finishing passes
Maintain rigid workholding
Control vibration
Optimize feed per tooth
Because magnesium machines easily, excellent surface finishes can often be achieved without excessive finishing operations.
Common Problems in Magnesium Machining
Despite its good machinability, several problems can occur.
| Problem | Possible Cause | Solution |
|---|---|---|
| Poor surface finish | Dull tool or vibration | Use sharp tools and improve rigidity |
| Excessive heat | Tool rubbing or improper parameters | Optimize feeds and cutting conditions |
| Chip buildup | Poor evacuation | Improve chip removal |
| Burr formation | Incorrect tool geometry | Optimize cutting tool and feed |
| Dimensional variation | Thin-wall deformation | Improve workholding |
| Excessive fine chips | Improper cutting conditions | Optimize tool geometry and cutting parameters |
| Tool marks | Runout or unstable machining | Check spindle, toolholder, and toolpath |
Controlling these factors helps manufacturers improve both productivity and component quality.
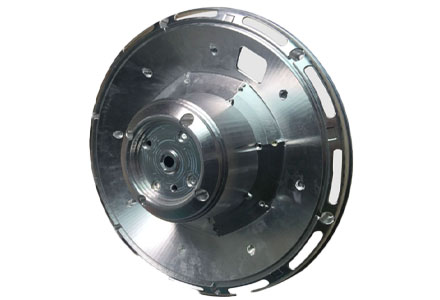
Magnesium Machining vs Aluminum Machining
Magnesium and aluminum are both widely used lightweight metals, but their machining characteristics are not identical.
| Property | Magnesium | Aluminum |
|---|---|---|
| Density | Very low | Low |
| Machinability | Excellent | Excellent |
| Cutting force | Very low | Low |
| Machining speed potential | High | High |
| Chip ignition concern | Higher | Lower |
| Tool wear | Generally low | Generally low |
| Weight reduction potential | Excellent | Good |
Magnesium is approximately one-third lighter than aluminum by volume, which makes it particularly attractive for applications where every gram matters.
However, magnesium machining requires more attention to chip handling and combustible-metal safety.
Applications of CNC Machined Magnesium Parts
Because of its low weight and excellent machinability, magnesium is used across many high-performance industries.
Aerospace
Magnesium components can reduce aircraft weight while maintaining sufficient mechanical strength.
Applications include brackets, housings, structural components, and equipment frames.
Automotive
Magnesium is used in lightweight automotive structures, transmission housings, steering components, electronic housings, and other weight-sensitive parts.
Electronics
Magnesium alloys are popular for lightweight electronics housings because they combine low weight, rigidity, dimensional stability, and electromagnetic shielding characteristics.
Medical Equipment
Precision Magnesium Alloy Machining can be used for medical device structures, equipment housings, and specialized mechanical components.
Robotics and Automation
Reducing moving mass can improve acceleration, positioning performance, and energy efficiency, making magnesium attractive for robotic and automated equipment.
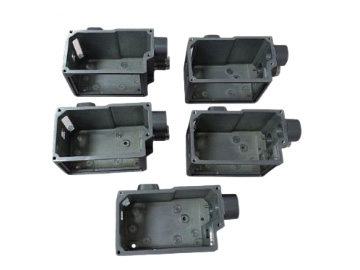
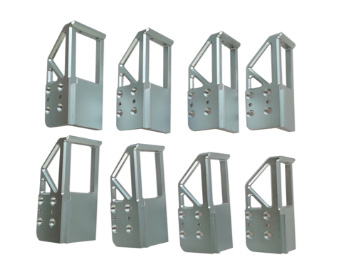
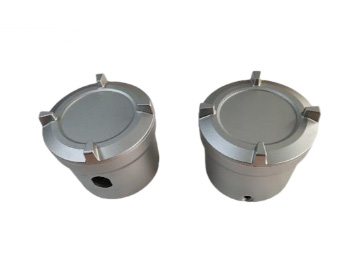
Choosing a Magnesium CNC Machining Manufacturer
When outsourcing magnesium machining services, buyers should evaluate more than machining capacity alone.
An experienced supplier should understand:
Magnesium alloy characteristics
CNC milling and turning
Thin-wall machining
Precision tolerances
Chip management
Combustible-metal safety
Surface finishing
Inspection and quality control
Manufacturers should also be capable of selecting machining strategies according to component geometry, production quantity, tolerance requirements, and final application.
For complex projects, early communication between design engineers and machining specialists can help improve manufacturability and reduce unnecessary production costs.
Frequently Asked Questions About Machining Magnesium
Is magnesium difficult to machine?
No. Magnesium is generally considered one of the easiest structural metals to machine. It requires relatively low cutting forces and allows high material removal rates.
Can magnesium be CNC machined?
Yes. CNC machining magnesium is widely used for precision components in aerospace, automotive, electronics, medical, and industrial applications.
Can you mill magnesium?
Yes. Magnesium milling can be performed using standard CNC machining centers with suitable tooling, cutting parameters, chip evacuation, and safety controls.
Can magnesium be turned on a CNC lathe?
Yes. Magnesium turning is commonly used to produce shafts, sleeves, rings, housings, and other rotational components.
Can magnesium be drilled?
Yes. Magnesium is relatively easy to drill. However, effective chip removal is especially important for deep holes.
Does magnesium catch fire during machining?
Solid magnesium parts do not normally ignite during properly controlled CNC machining. The greater risk comes from fine magnesium chips, dust, or powder, particularly when they accumulate or encounter an ignition source.
What tools are used for magnesium machining?
Sharp carbide tools are commonly used for production CNC machining. Tool geometry should promote clean cutting and efficient chip evacuation.
Understanding how to machine magnesium requires more than simply selecting high cutting speeds.
Magnesium offers excellent machinability, low cutting resistance, fast material removal, and good surface quality, making it highly suitable for modern CNC manufacturing. CNC milling, turning, and drilling can all be used efficiently to manufacture precision magnesium components.
However, successful magnesium alloy machining depends on sharp cutting tools, appropriate machining parameters, effective chip evacuation, correct workholding, heat control, and strict magnesium machining safety procedures.
When these factors are properly controlled, magnesium CNC machining can provide an efficient solution for lightweight, high-precision components used in aerospace, automotive, electronics, medical equipment, robotics, and other demanding industries.


